 English
We firmly believe that true manufacturing value lies not only in superior product performance but also in our responsibility to the environment, our commitment to society, and our long-term vision for...
Leisure Sports Materials
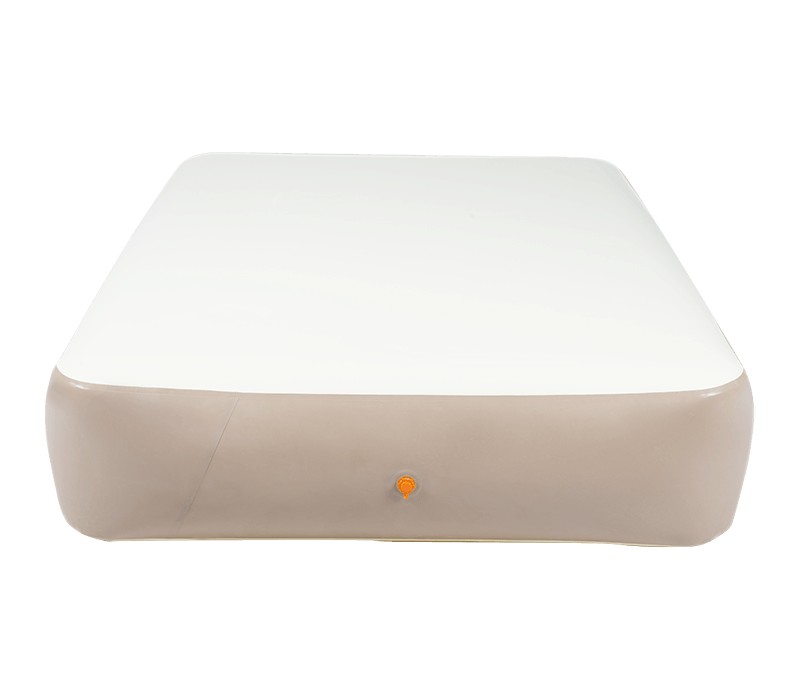
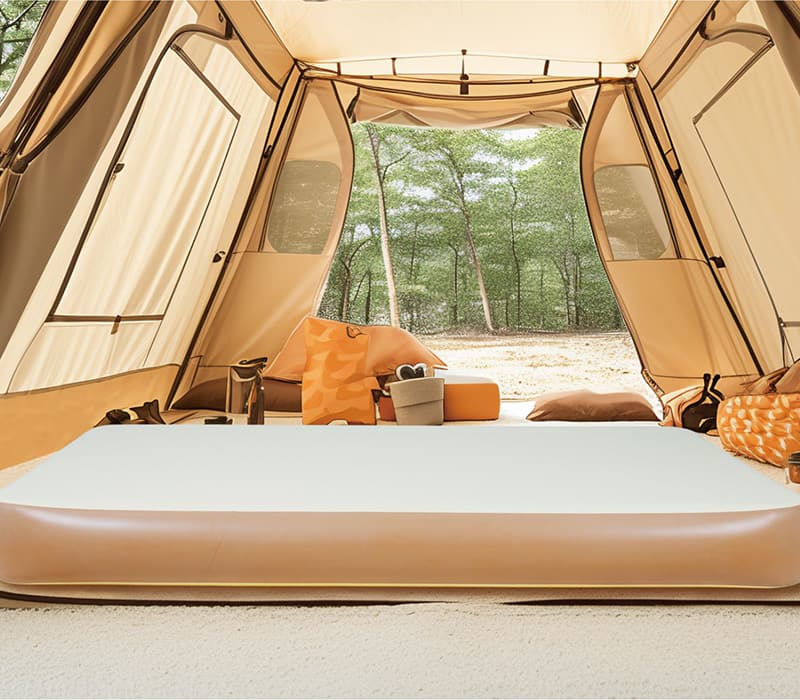
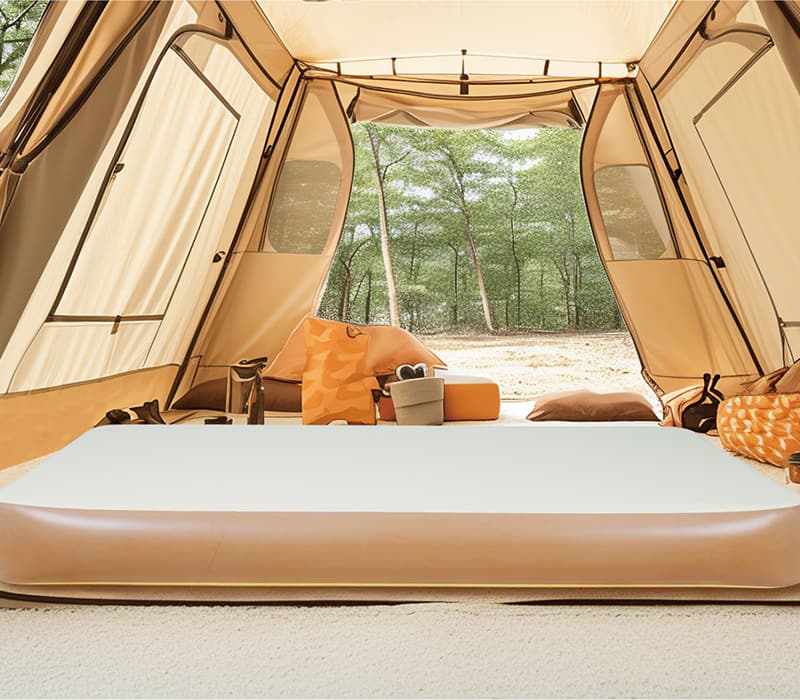
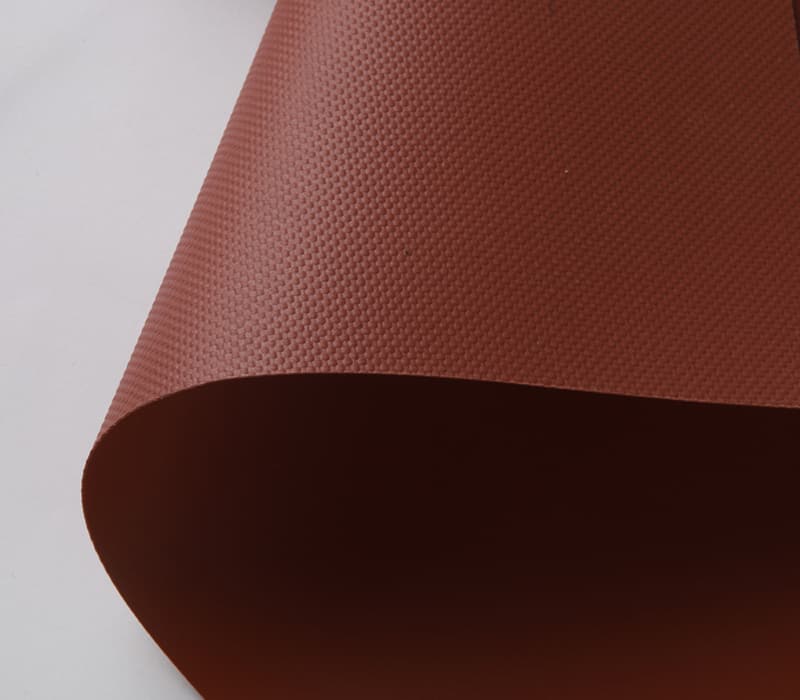
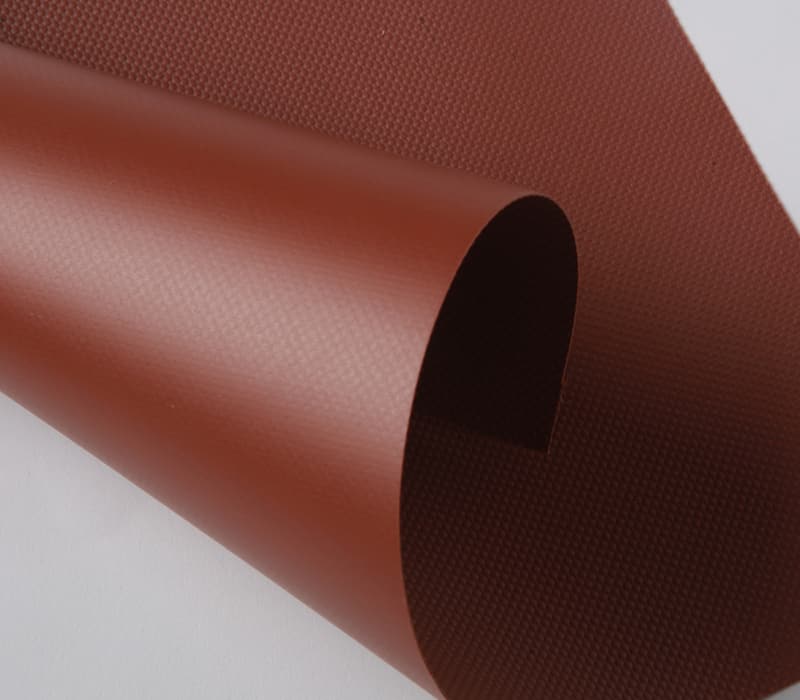
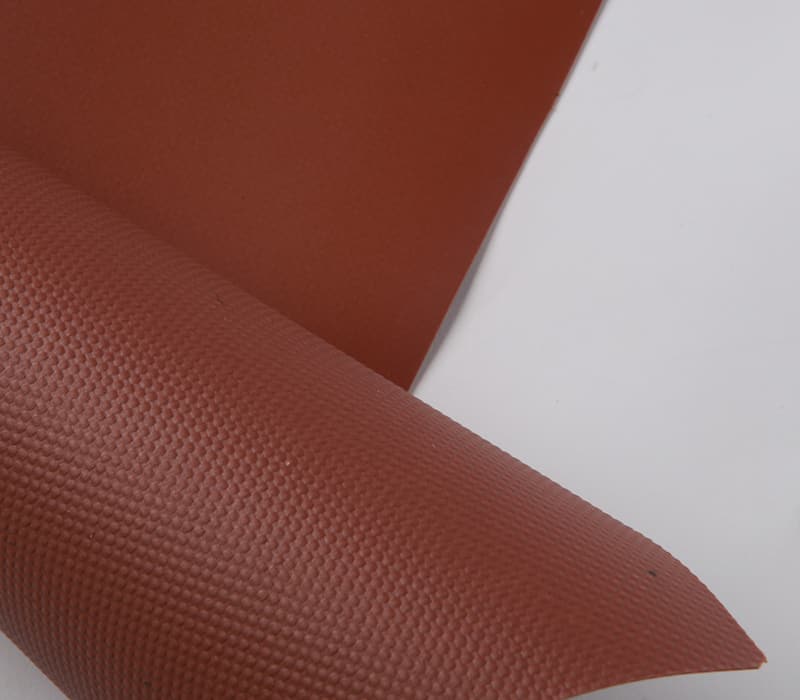
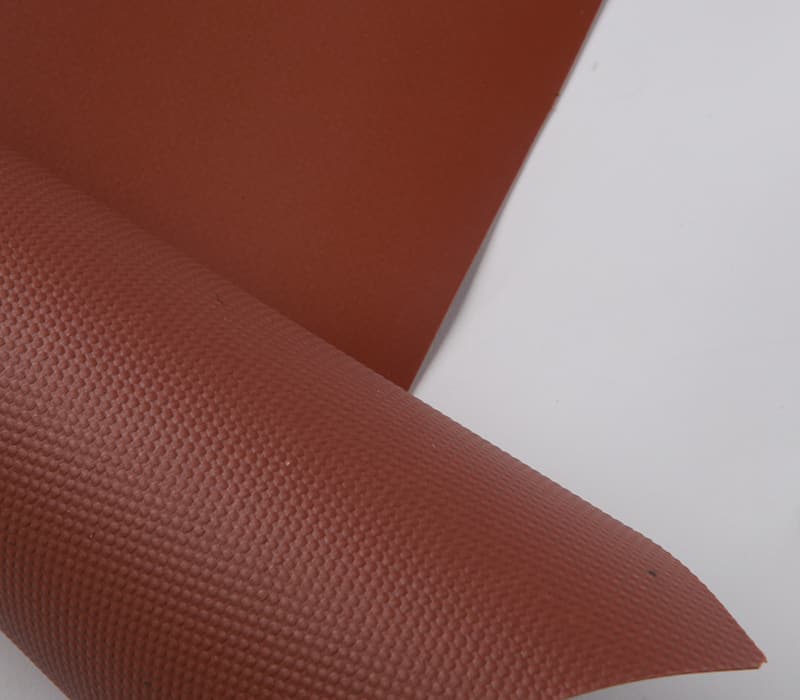
Leisure & Sports Materials for Inflatable Structures and Recreation Equipment
Leisure & Sports Materials are reinforced textiles and flexible composites developed for inflatable recreation products, water-sports equipment, training surfaces, floating platforms, and other air-supported structures. Depending on the construction, these materials may combine woven textile layers, internal connecting yarns, polymer coatings, laminated films, and surfaces designed for compatible joining processes.
MSD develops drop stitch material for inflatable products that need controlled thickness and a comparatively flat profile after inflation. Thousands of internal yarns connect the upper and lower fabric layers. As air pressure increases inside the finished chamber, these yarns restrict outward expansion and help the product retain its intended geometry.
Drop stitch material must be assessed as one part of the complete inflatable structure. Textile strength alone cannot define air retention, working pressure, rigidity, seam integrity, or service life. Sidewalls, surface layers, valves, joining parameters, reinforcements, product dimensions, load distribution, and operating conditions all contribute to finished performance.
Material Definition, Structure, and Working Principle
This section introduces the materials included in the category, explains the construction of drop stitch composites, and describes how internal yarns help create a stable inflatable surface.
What Is the Leisure & Sports Materials Category?
The Leisure & Sports Materials category covers coated, laminated, textile-based, and structurally reinforced materials created for recreational, athletic, outdoor, water-based, and inflatable products.
According to their construction, these materials may provide:
- Textile reinforcement
- Air-retaining surface layers
- Dimensional control
- Tensile support
- Surface protection
- Flexibility
- Print compatibility
- Welding or adhesive-bonding compatibility
- Decorative colors and textures
- Resistance to repeated rolling and unfolding
Common applications include:
- Inflatable paddle boards
- Inflatable docks
- Floating platforms
- Gymnastics and training mats
- Inflatable watercraft components
- Air-supported furniture
- Recreation equipment
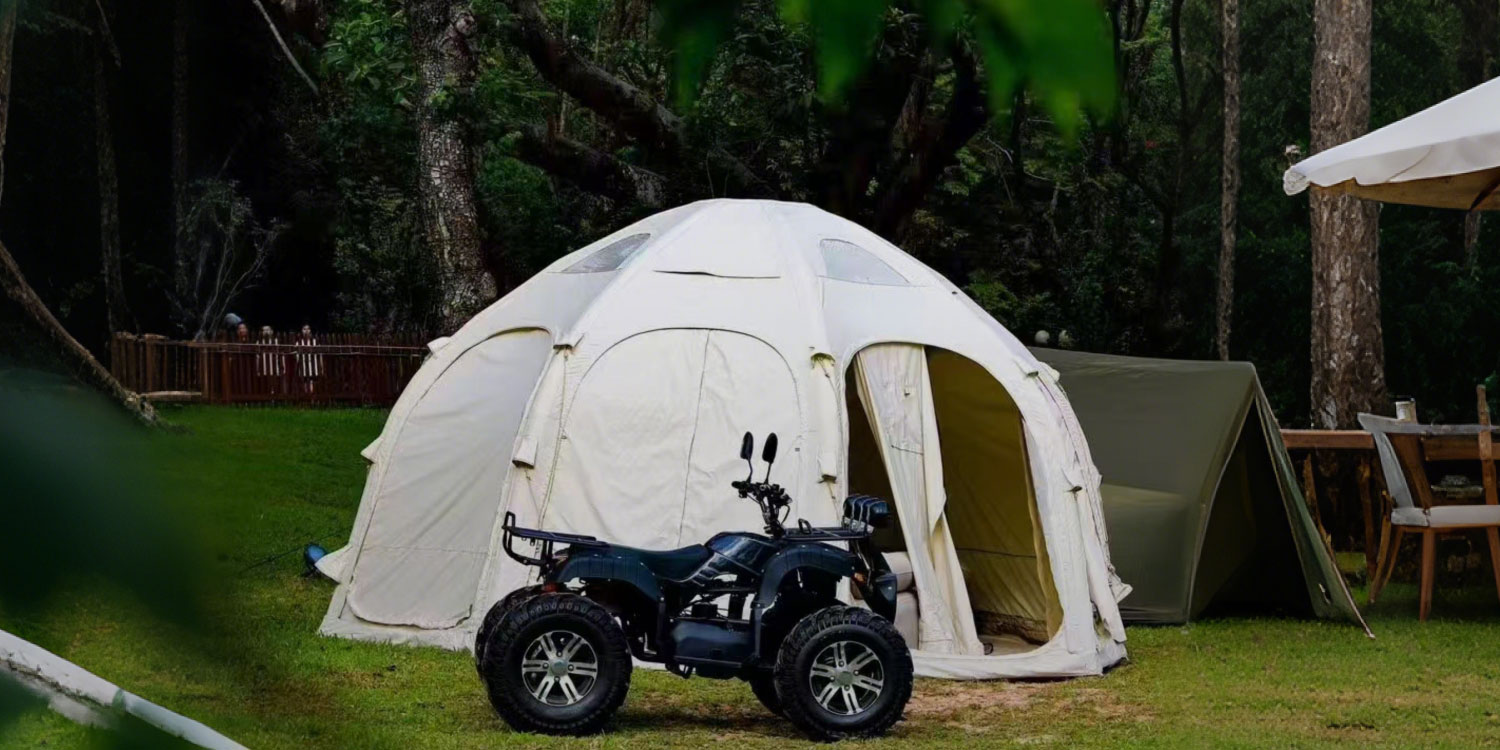
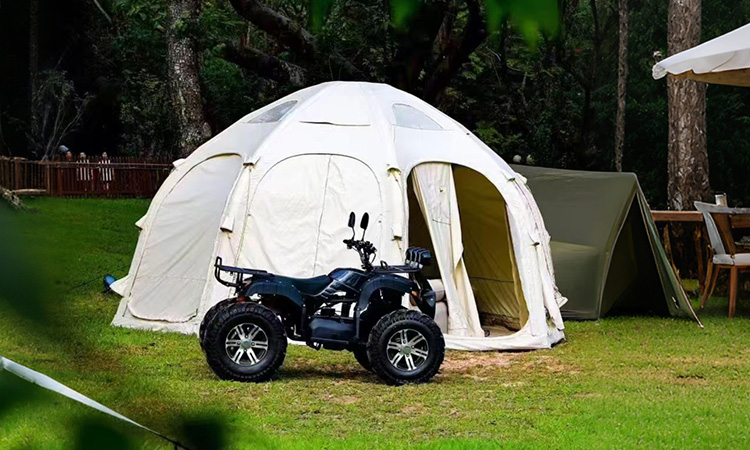
- Inflatable shelters
- Flexible structural air chambers
This category represents a field of application rather than one universal material. Each construction has its own textile design, surface composition, joining response, thickness, weight, and environmental suitability.
Material selection should therefore begin with the intended inflatable structure. Product geometry, operating pressure, joining process, load conditions, water exposure, storage method, and applicable safety requirements all need to be considered.
What Is Drop Stitch Material?
Drop stitch material is a three-dimensional textile composite made from two parallel fabric surfaces connected by a dense network of internal yarns. The controlled length of these yarns limits how far the outer surfaces can separate when the completed air chamber is inflated.
A typical drop stitch construction contains:
- An upper textile layer
- A lower textile layer
- Internal connecting yarns
- Coated or laminated outer surfaces
- Sidewall material added during fabrication
- Welded or adhesively bonded seams
- Valves and application-specific components
Drop stitch material is normally supplied as a semi-finished structural composite. It does not become a completed airtight product until panels, perimeter sidewalls, seams, valves, reinforcements, handles, and other accessories have been correctly integrated.
Its behavior differs from that of an unsupported inflatable chamber. A conventional air chamber naturally tends to become rounded as internal pressure rises. In a drop stitch structure, the connecting yarns restrict expansion, allowing the product to maintain a defined thickness and a flatter surface.
How Does Drop Stitch Material Work?
When air enters a sealed drop stitch chamber, pressure pushes the upper and lower surfaces away from one another. As the distance increases, the internal yarns become tensioned. Their controlled length prevents further expansion and helps stabilize the shape.
The geometry and rigidity of the inflated product are influenced by:
- Length of the connecting yarns
- Yarn density
- Yarn distribution
- Yarn alignment
- Stability of the yarn connections
- Construction of the upper and lower textiles
- Coating or lamination system
- Inflated thickness
- Product length and width
- Sidewall design
- Seam geometry
- Valve installation
- Internal pressure
- Load position and distribution
Pressure data should never be separated from product design and fabrication. A small material specimen, a welded chamber, and a full-size inflatable structure can behave differently even when made from the same base material.
Temperature also matters. Changes in environmental temperature can alter internal pressure, material flexibility, and dimensional response. Pressure validation should therefore reflect the conditions expected during use and storage.
Main Components of Drop Stitch Material
Every part of a drop stitch composite has a particular role. Finished performance comes from the interaction between these parts rather than from one layer working alone.
| Component | Primary Function | Technical Considerations |
| Internal yarns | Connect the outer surfaces and control inflated thickness | Length, density, alignment, tensile response, connection stability |
| Upper textile layer | Supports the upper surface and anchors connecting yarns | Fabric density, dimensional stability, surface uniformity |
| Lower textile layer | Supports the lower surface and anchors connecting yarns | Textile structure, flatness, coating compatibility |
| Outer surface system | Supports air retention, protection, appearance, and fabrication | Layer adhesion, thickness, flexibility, joining response |
| Sidewall material | Closes the perimeter of the air chamber | Flexibility, corner behavior, seam compatibility |
| Seams | Connect panels, sidewalls, and reinforced sections | Process settings, seam width, geometry, pressure response |
| Valve | Controls inflation and deflation | Position, installation, sealing, flow, material compatibility |
A change to any one component may affect weight, rigidity, air retention, appearance, packability, or processing. For example, a different surface layer may require new welding settings, while a change in yarn length alters the inflated thickness.
Internal Connecting Yarns
The internal yarn network defines the basic behavior of drop stitch material. Yarn length helps establish the distance between the outer surfaces, while density and distribution affect how pressure and applied loads are transferred through the structure.
Important yarn characteristics include:
- Yarn material
- Yarn count
- Yarn length
- Yarn density
- Yarn alignment
- Connection pattern
- Tension consistency
- Response to repeated loading
Uneven yarn length or irregular distribution may produce local changes in thickness, surface shape, or load response. Inspection should therefore include inflated samples rather than relying only on the appearance of uninflated roll material.
The way the yarns connect with the upper and lower textiles is equally important. Connection stability can influence the product’s response to repeated inflation, concentrated loads, and long pressure-hold periods.
Upper and Lower Textile Layers
The upper and lower textile layers support the internal yarns and provide the foundation for coating or lamination.
Relevant characteristics include:
- Textile construction
- Yarn strength
- Fabric density
- Surface consistency
- Dimensional stability
- Thermal response
- Coating adhesion
- Lamination compatibility
- Resistance to production tension
These textile layers provide reinforcement but are not independently airtight. Air retention depends on the outer polymer system, sidewalls, seams, valve installation, and the integrity of the completed chamber.
Surface consistency also matters during later fabrication. Variations in textile density or flatness may become visible after coating, printing, or inflation.
Coated or Laminated Outer Surfaces
The outer surface system contributes to air retention, protection, appearance, cleanability, print response, and joining compatibility.
Depending on the material grade, the construction may contain:
- PVC-based surface layers
- Application-specific polymer coatings
- Laminated films
- Reinforced composite layers
- Colored finishes
- Print-compatible surfaces
- Smooth or textured finishes
Surface formulation and thickness can influence flexibility, abrasion response, welding behavior, adhesive interaction, and packability.
The exact composition should be checked through the technical information for the selected material construction. A joining process developed for one surface system should not automatically be transferred to another.
Sidewalls, Seams, and Valves
Drop stitch panels do not form a closed chamber on their own. Sidewall strips are added around the perimeter to connect the upper and lower surfaces and seal the inflatable structure.
The sidewall system should be assessed for:
- Compatibility with panel surfaces
- Flexibility around corners
- Welding or bonding temperature
- Seam width
- Layer adhesion
- Repeated inflation response
- Local stress distribution
- Valve integration
- Repair method
Corners, valves, handles, fins, straps, rings, and attachment mounts often carry concentrated stress. These areas may need additional patches, wider seams, modified geometry, or application-specific reinforcement.
Valve position also affects inflation, deflation, accessibility, local stress, and the usable surface. Installation should be checked for leakage and for any distortion around the valve opening.
Manufacturing, Performance, and Fabrication
Drop stitch material combines three-dimensional textile engineering with polymer coating or lamination. Consistent production requires careful control of yarn geometry, textile formation, layer adhesion, thermal processing, surface quality, and roll preparation.
How Is Drop Stitch Material Manufactured?
The manufacturing process generally covers yarn preparation, three-dimensional textile formation, coating or lamination, stabilization, inspection, and roll preparation.
Yarn and textile preparation
Yarn specifications, alignment, and tension are controlled before the three-dimensional textile is formed.
Important variables include:
- Yarn specification
- Yarn tension
- Yarn alignment
- Feed consistency
- Textile density
- Uniformity of the upper and lower surfaces
Stable yarn feeding helps maintain consistent thickness and surface shape after inflation. Variations at this stage may become difficult to correct after the textile has been coated or laminated.
Three-dimensional textile formation
The upper and lower textile surfaces are formed together with the connecting yarn network. Yarn length and arrangement establish the internal geometry of the material.
Production control may include:
- Distance between the outer layers
- Connecting-yarn consistency
- Textile density
- Surface flatness
- Yarn attachment
- Width stability
- Visible structural variation
The material may appear compressed when supplied in roll form. Its three-dimensional structure becomes more apparent after it is fabricated into a chamber and inflated.
Coating or lamination
Compatible polymer layers are applied to the textile structure to create a flexible composite with the required surface and fabrication properties.
Process variables may include:
- Surface preparation
- Coating or film thickness
- Application uniformity
- Temperature
- Pressure
- Line speed
- Layer adhesion
- Cooling conditions
- Finished appearance
Coating and lamination must be controlled across the working width. Uneven processing may affect appearance, bonding, welding response, dimensions, or air retention.
Stabilization and inspection
After surface processing, the composite may require controlled cooling, curing, or conditioning. The precise method depends on the polymer system and construction.
Inspection may cover:
- Material width
- Total thickness
- Area weight
- Surface appearance
- Connecting-yarn distribution
- Layer adhesion
- Dimensional behavior
- Color consistency
- Edge quality
- Roll condition
A representative inflated specimen can also help reveal thickness variation, local deformation, and irregularities that may not be obvious in flat roll material.
Technical Properties of Leisure & Sports Materials
Technical values should always identify what was tested. A textile layer, coated composite, welded specimen, sidewall joint, and completed inflatable product represent different test objects and should not be treated as interchangeable.
Tensile strength
Tensile strength describes the material’s response to pulling force under defined test conditions.
Results can be affected by:
- Test direction
- Specimen width
- Conditioning
- Test speed
- Grip method
- Textile construction
- Surface-layer construction
Textile composites may behave differently in their principal directions. Results should therefore identify the tested orientation and applicable standard.
Tensile data can support material comparison, but it does not establish finished-product pressure capacity on its own.
Tear resistance
Tear resistance measures how damage progresses after a cut or tear has already started. It is different from tensile strength, puncture response, seam strength, and abrasion behavior.
Areas requiring particular attention may include:
- Valve openings
- Handles
- Attachment points
- Panel edges
- Hardware openings
- Corners
- Reinforcement boundaries
Local geometry can concentrate stress even when the base material has suitable tear properties.
Peel adhesion
Peel adhesion describes the bond between coated, laminated, or otherwise connected layers.
It can be influenced by:
- Surface preparation
- Polymer compatibility
- Processing temperature
- Pressure
- Curing
- Sample conditioning
- Water exposure
- Heat exposure
- Repeated folding
Peel results should identify the sample structure, test direction, test speed, conditioning method, and relevant layer interface.
A strong initial bond may change after water exposure, thermal cycling, or repeated packing. Conditioning should reflect the intended application where possible.
Air retention
Air retention depends on the complete inflatable chamber, including:
- Outer surface layers
- Sidewall strips
- Panel seams
- Valve installation
- Accessory connections
- Reinforcement details
- Fabrication parameters
- Surface damage
Material permeability information is useful, but it does not replace leakage testing on welded joints or representative finished products.
Pressure-hold testing should define the initial pressure, hold time, temperature, measurement method, and permissible variation. Temperature changes during the test can affect pressure readings and need to be considered.
Pressure response
Pressure response describes how an inflatable structure behaves as internal pressure increases or is maintained over time.
Evaluation may include:
- Dimensional change
- Surface flatness
- Local deformation
- Seam response
- Leakage
- Valve behavior
- Structural stability
A representative test should reflect:
- Product length and width
- Inflated thickness
- Sidewall construction
- Seam geometry
- Valve type
- Conditioning temperature
- Hold time
- Safety controls
Working pressure and validation pressure are not the same. Any stated value should identify whether it relates to normal use, process testing, validation, or another defined condition.
Dimensional stability
Dimensional stability matters throughout:
- Coating
- Lamination
- Printing
- Cutting
- Welding
- Adhesive bonding
- Inflation
- Cooling
- Storage
Uncontrolled movement can affect panel matching, seam position, printed graphics, inflated thickness, and final geometry.
The material’s response should be considered in both roll processing and the completed inflatable structure.
Puncture and abrasion response
Puncture and abrasion represent different forms of damage.
Puncture response concerns concentrated contact from a pointed or sharp object.
Abrasion response concerns gradual surface change caused by repeated rubbing.
Both can be influenced by:
- Surface-layer composition
- Layer thickness
- Textile reinforcement
- Test load
- Contact material
- Cycle count
- Temperature
- Sample conditioning
Results should be linked to a stated test method. A favorable abrasion result does not establish resistance to puncture, cutting, impact, or seam damage.
Flexibility and packability
Inflatable recreation equipment is often deflated, rolled, folded, transported, stored, and reopened. The composite needs suitable flexibility for these repeated handling cycles.
Evaluation may consider:
- Surface cracking
- Coating whitening
- Layer separation
- Permanent creases
- Loss of flexibility
- Distortion after storage
- Behavior at low temperature
Repeated-fold testing can provide useful information when the finished product will be packed frequently or stored under pressure.
Environmental response
Depending on the intended use, evaluation may include:
- Freshwater exposure
- Saltwater exposure
- High humidity
- Elevated temperature
- Low-temperature handling
- Sunlight
- Repeated inflation
- Repeated folding
- Contact with cleaning substances
- Storage pressure
Outdoor suitability should be based on the selected material grade and supporting test information. An indoor construction should not automatically be considered suitable for prolonged exterior or marine exposure.
Converting and Fabrication Methods
Drop stitch material should be evaluated using the equipment, joint design, and process settings intended for the finished product.
Cutting
Accurate cutting supports panel alignment, symmetry, seam placement, and finished dimensions.
A cutting plan should consider:
- Material direction
- Panel dimensions
- Seam allowance
- Valve location
- Reinforced areas
- Printed graphics
- Edge quality
- Tool condition
Cut edges should be checked for fraying, distortion, surface-layer separation, and dimensional accuracy before joining begins.
Printing
Applicable surfaces may support compatible printing methods for decoration, product identification, instructions, markings, or graphics.
A print trial should assess:
- Ink adhesion
- Color appearance
- Image definition
- Curing conditions
- Surface response
- Flexibility after printing
- Water exposure
- Cleaning response
- Influence on welding or bonding areas
Printed graphics should be planned around seams, valves, handles, and folds. Ink or coating within a joining zone may alter seam formation or adhesion.
Welding
Depending on the outer surface construction, suitable methods may include high-frequency, hot-air, thermal, or another validated welding process.
Welding assessment should cover:
- Seam strength
- Seam width
- Surface appearance
- Heat marks
- Layer distortion
- Air retention
- Corner response
- Process repeatability
- Performance after conditioning
Parameters established for one thickness or coating system may not be suitable for a different construction. Equipment settings should be validated using representative joints.
Adhesive bonding
Some inflatable products use adhesive bonding for sidewalls, reinforcement patches, accessories, attachment points, or repair sections.
Bond performance can be affected by:
- Surface preparation
- Adhesive chemistry
- Application quantity
- Open time
- Contact pressure
- Curing conditions
- Temperature
- Water exposure
- Direction of loading
The adhesive and composite should be tested together. Representative joints should reproduce the intended overlap, surface treatment, curing time, and service conditions.
Edge and attachment reinforcement
Handles, fins, valves, straps, rings, corners, and connection points may experience loads much higher than those on surrounding areas.
Reinforcement can involve:
- Additional material layers
- Local patches
- Wider seams
- Rounded transitions
- Modified component geometry
- Increased bonding area
- Load-spreading structures
The reinforcement itself can create stress at its edge, so the complete detail should be tested rather than evaluating only the added patch.
Applications of Leisure & Sports Materials
Drop stitch composites can be used in a range of inflatable products where controlled thickness, packability, and pressure-supported shape are required.
Inflatable paddle boards
Drop stitch material can form the pressure-supported body and deck of an inflatable paddle board.
Important factors include:
- Board dimensions
- Inflated thickness
- Internal yarn construction
- Outer surface system
- Rail and sidewall design
- Valve location
- Fin attachment
- Handle reinforcement
- Surface texture
- Intended pressure
- Water and sunlight exposure
Board stiffness and stability depend on the complete construction. Material thickness, pressure, width, outline, rail design, and load position all influence how the board behaves on water.
The areas around fins, valves, handles, and deck attachments may require dedicated reinforcement and testing.
Inflatable docks and floating platforms
Floating platforms can use drop stitch construction to provide a comparatively flat surface for walking, sitting, connecting equipment, or supporting distributed loads.
Material and product assessment should consider:
- Platform dimensions
- Inflated thickness
- Load distribution
- Connection points
- Surface grip
- Sidewall seams
- Repeated water exposure
- Attachment hardware
- Inflation and deflation cycles
- Storage method
A large platform responds differently to pressure and loading than a small panel. Full-size or representative structural testing is valuable where geometry has a major influence.
Gymnastics and training mats
Drop stitch material can be used for inflatable training surfaces requiring controlled thickness and pressure-adjustable response.
Finished performance may be influenced by:
- Mat length and width
- Inflated thickness
- Internal structure
- Operating pressure
- Surface friction
- Edge design
- Rebound behavior
- User load
- Floor condition
Safety and performance testing should reflect the intended activity, user group, installation surface, and applicable requirements.
Pressure changes can alter firmness and rebound. The recommended inflation method should therefore be clearly defined for the finished product.
Inflatable watercraft components
Drop stitch panels may be used in floors, seats, side structures, or other compatible sections of inflatable watercraft.
Evaluation should cover:
- Buoyancy design
- Panel geometry
- Sidewall construction
- Seams
- Valves
- Reinforcement
- Water exposure
- Saltwater contact
- Applicable safety requirements
A material’s use in one type of watercraft component does not automatically establish suitability for another. Load, geometry, pressure, and attachment details may be substantially different.
Air-supported furniture
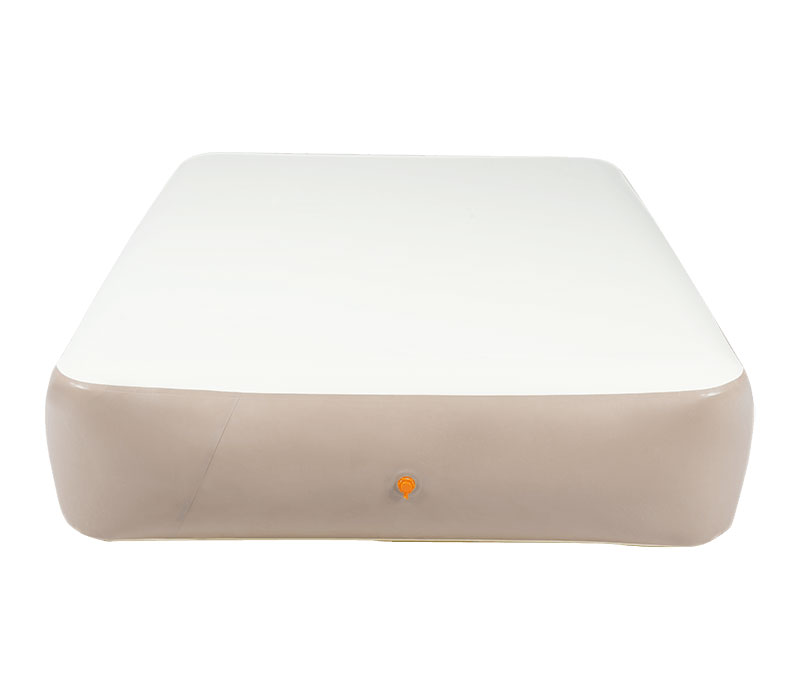
Selected drop stitch constructions can support inflatable benches, beds, tables, seating components, and temporary furniture forms.
Product stability is influenced by:
- Geometry
- Internal pressure
- Load location
- Floor contact
- Seam arrangement
- Accessory connections
- Surface friction
- Repeated loading
Concentrated loads near an edge or corner can create a different response from evenly distributed weight. Representative testing should reflect normal use.
Outdoor recreation structures
Leisure and sports composites may also be used in compatible play, camping, event, and outdoor recreation products.
Each application requires a defined review of:
- Internal pressure
- Static and dynamic loads
- Environmental exposure
- User contact
- Joining method
- Attachment points
- Installation conditions
- Safety requirements
Material selection should follow the actual structure rather than relying solely on experience from a different inflatable product.
How to Select Leisure & Sports Materials
A reliable selection process begins with the finished product and works back toward the material construction, joining method, and required test plan.
1. Define the application
Identify whether the material will form:
- A paddle board
- A floating platform
- A training mat
- A watercraft component
- Inflatable furniture
- An air-supported recreation structure
This initial definition helps establish the required geometry, pressure, surface, load, and environmental criteria.
2. Establish product geometry
Confirm:
- Length
- Width
- Inflated thickness
- Panel shape
- Corner radius
- Sidewall arrangement
- Valve position
- Attachment points
Geometry affects material stress, surface flatness, seam layout, stiffness, and load distribution.
Long or wide products may require a different structural assessment from small specimens, even when the same material is used.
3. Define pressure conditions
Pressure planning should cover:
- Intended working pressure
- Inflation procedure
- Pressure changes caused by temperature
- Validation method
- Pressure-hold period
- Deflation procedure
- Safety controls
Material data should not be presented as a finished-product pressure rating without supporting structural validation.
4. Review load conditions
Possible load types include:
- Static load
- Dynamic load
- Distributed load
- Concentrated load
- Repeated loading
- Impact
- Attachment-point stress
A floating platform carrying evenly distributed weight may behave differently when the same total load is concentrated in one small area.
5. Select the surface construction
The outer surface system should be chosen with reference to:
- Air-retention requirements
- Weight target
- Flexibility
- Abrasion exposure
- Printing requirements
- Welding response
- Adhesive-bonding response
- Surface texture
- Cleaning method
- Environmental conditions
No single surface construction is ideal for every inflatable product. The required balance depends on use, fabrication, transport, and storage.
6. Confirm the joining process
The material should be evaluated with the proposed welding or adhesive system.
Test specimens should reproduce:
- Seam width
- Overlap geometry
- Temperature
- Pressure
- Dwell time
- Surface preparation
- Curing conditions
- Cooling method
- Direction of loading
Flat seam specimens may be supplemented by corner, sidewall, valve, or reinforced-joint samples where these details are critical.
7. Review the service environment
Define whether the product will encounter:
- Indoor conditions
- Exterior exposure
- Freshwater
- Saltwater
- Direct sunlight
- High temperatures
- Low temperatures
- Frequent cleaning
- Repeated packing
- Long storage periods
Exposure conditions can affect flexibility, adhesion, color, surface appearance, and pressure. Storage conditions should be considered alongside active use.
8. Complete a fabrication trial
A representative fabrication trial can assess:
- Cutting accuracy
- Printing
- Welding or adhesive bonding
- Valve installation
- Reinforcement details
- Inflation
- Surface shape
- Air retention
- Seam response
- Finished dimensions
The closer the trial is to the actual product geometry and process, the more useful the findings will be.
MSD Manufacturing Capabilities and FAQs
MSD treats leisure and sports materials as integrated textile-composite systems. Material development connects the internal yarn structure with surface processing, fabrication behavior, and the requirements of the finished inflatable product.
Why Choose MSD Leisure & Sports Materials?
MSD develops Leisure & Sports Materials with attention to textile construction, internal yarn consistency, surface-layer composition, dimensional control, layer adhesion, and converting compatibility. The category focuses on drop stitch materials for inflatable recreation products, water sports, training equipment, floating platforms, and related air-supported structures.
Rather than assessing drop stitch material as a single textile layer, MSD considers the relationship between internal yarns, upper and lower fabrics, coated or laminated surfaces, joining response, inflated geometry, and application conditions.
Relevant capabilities include:
- Drop stitch structural development
- Internal yarn-geometry control
- Textile-surface management
- Coating and lamination integration
- Thickness and width control
- Surface-appearance inspection
- Layer-adhesion evaluation
- Color and finish development
- Print-compatibility assessment
- Welding-response assessment for applicable constructions
- Dimensional-stability evaluation
- Roll and edge inspection
- Application-focused material development
- Technical documentation for relevant material grades
MSD also evaluates how material construction interacts with cutting, printing, welding, adhesive bonding, inflation, water exposure, repeated folding, and storage.
Where a project requires a defined pressure condition, thickness, surface system, joining method, or mechanical value, the supporting information should correspond to the selected construction and stated test procedure.
Frequently Asked Questions About Leisure & Sports Materials
Why does drop stitch material remain relatively flat?
Internal yarns connect the upper and lower surfaces and limit the distance between them. As the chamber is inflated, these yarns become tensioned and reduce uncontrolled outward expansion.
The resulting surface is comparatively flat, although final shape also depends on yarn consistency, product geometry, sidewalls, seams, and pressure.
Is drop stitch material airtight by itself?
Not as a completed product. Air retention depends on the coated or laminated surfaces, sidewalls, seams, valve installation, reinforcement details, and fabrication process.
The material should be evaluated through seam samples and a representative finished chamber.
Does a higher area weight always create a stronger structure?
No. Area weight provides useful construction information, but it does not independently define strength or product performance.
Yarn geometry, textile properties, layer adhesion, surface composition, seams, valves, reinforcements, dimensions, and product design also affect the final structure.
Can drop stitch material be printed?
Applicable surfaces may support compatible printing systems.
A print trial should evaluate ink adhesion, image definition, curing, flexibility, water exposure, cleaning response, and possible effects on welding or bonding zones.
Can drop stitch material be welded?
Compatible surface constructions may support high-frequency, hot-air, thermal, or another validated welding method.
Suitability depends on the polymer surface, film or coating thickness, equipment, temperature, pressure, dwell time, seam geometry, and cooling conditions.
What is the difference between tensile strength and tear resistance?
Tensile strength describes how a specimen responds when pulled under a defined load. Tear resistance describes how existing damage progresses through the material.
The two properties use different test approaches and should not be treated as equivalent.
Can drop stitch material be used in saltwater?
Suitability depends on the complete product construction, including surface layers, seams, valves, accessories, reinforcements, and expected exposure time.
Representative joints and finished samples should be evaluated under conditions that reflect the intended marine environment.
Leisure & Sports Materials bring together textile engineering, polymer surface technology, and inflatable-product fabrication. Within a drop stitch structure, internal connecting yarns control expansion, while the outer textiles and coated or laminated surfaces contribute to shape, protection, air retention, and joining.
Reliable performance depends on the complete structure. Yarn geometry, outer layers, sidewalls, seams, valves, reinforcements, pressure, dimensions, loading, fabrication settings, and environmental exposure all influence how the finished product behaves.
MSD Leisure & Sports Materials support drop stitch structures for inflatable recreation products, water-sports equipment, training mats, floating platforms, watercraft components, air-supported furniture, and related applications.
-

+86-(0)573-87985868
-

+86-(0)573-89237968
-

-

NO.11 Hongqi Road, warp knitting industrial park of Haining City, Zhejiang Province, China
Copyright © Zhejiang MSD Group Share Co., Ltd. All Rights Reserved.
Leisure Sports Materials Manufacturer